EN

Custom 6061 Aluminum Progressive Stamped Components
This page documents actual aluminum components manufactured by Zhengna Technology. The confirmed product record is aluminum alloy 6061 at 1.5 mm thickness, formed with progressive die tooling and stamping operations. The specified post-process condition is cleaning only, with no electroplating. Dimensional inspection uses a 2D optical measuring system. Quotation review can begin from a controlled drawing or a physical sample.
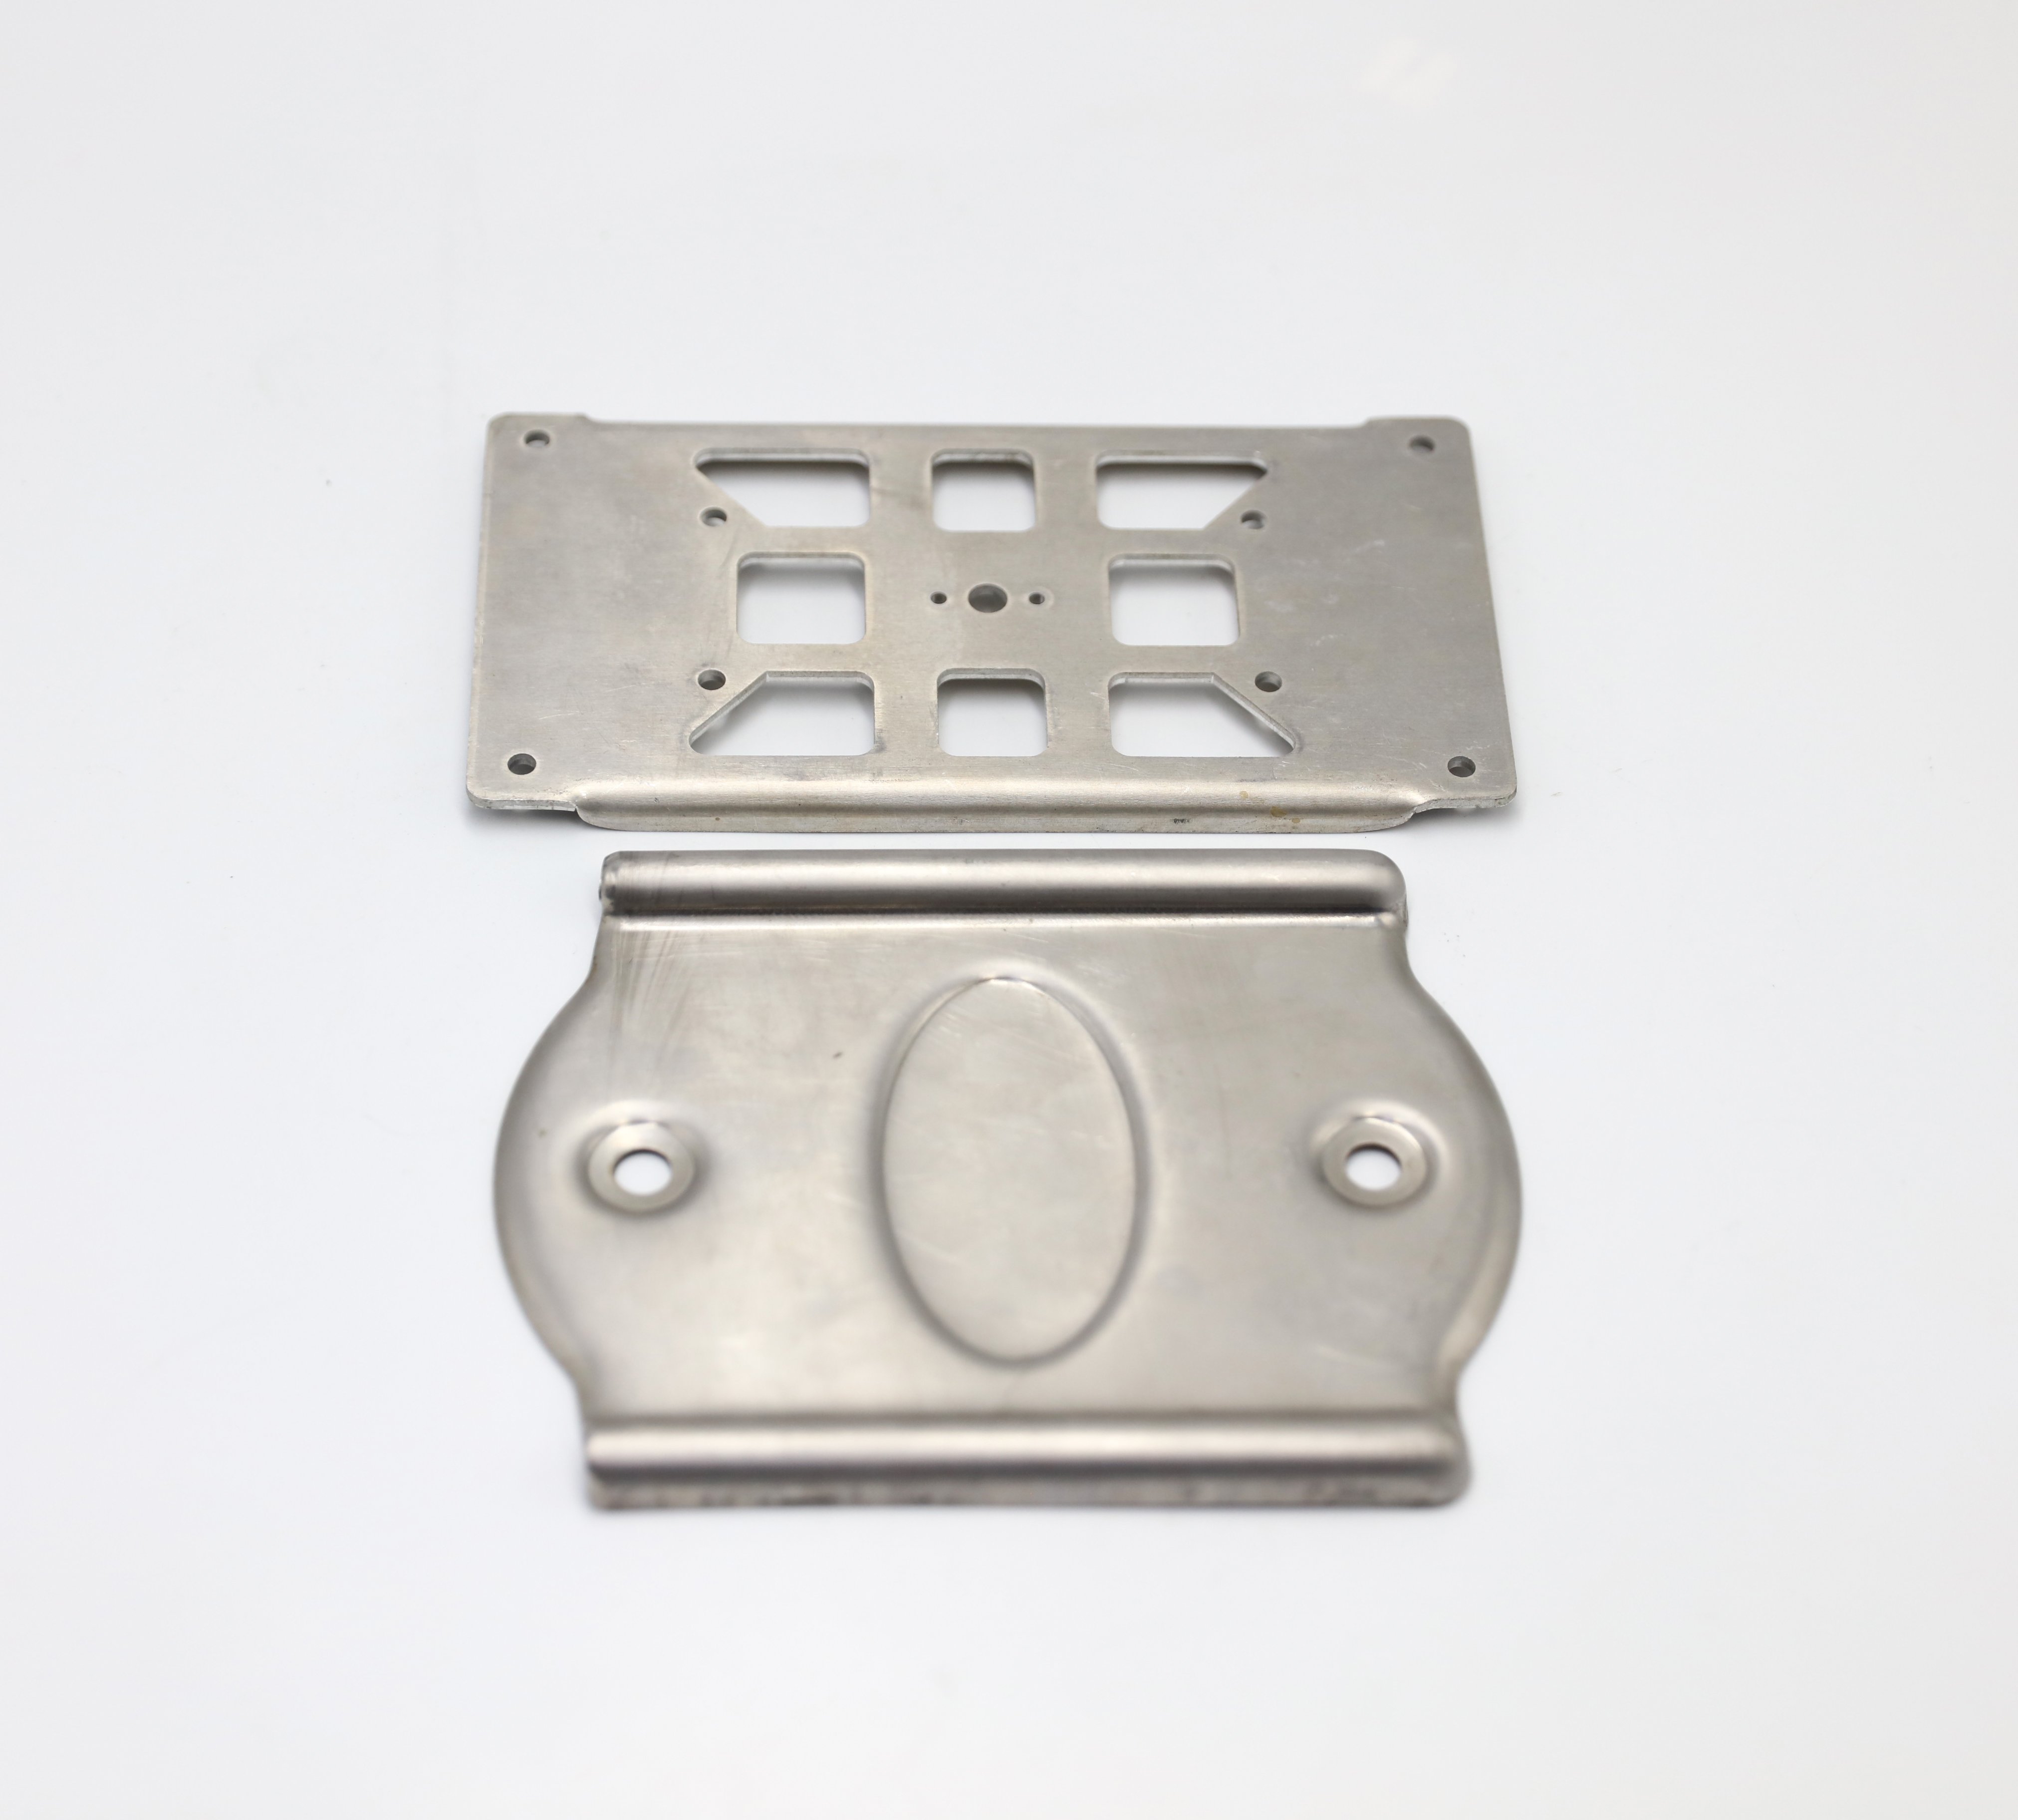
The photograph shows two stamped and formed components. One has a rectangular outline, multiple punched openings and a formed edge. The other has round holes, a central oval formed feature and rolled or formed edges. These visible features help identify the manufacturing family, but the photograph does not establish dimensions, tolerances, material temper, acceptance results, application or production volume.
What the Current Product Evidence Establishes
| Item | Confirmed for this product page | Still controlled by the RFQ |
|---|---|---|
| Product scope | Custom aluminum stamped and formed components | Part name, assembly function and end use |
| Material | Aluminum alloy 6061 | Temper, material standard and document requirements |
| Thickness | 1.5 mm | Thickness tolerance and local thinning limits |
| Manufacturing route | Progressive die tooling with stamping and forming | Station sequence, press interface, strip layout and tooling responsibility |
| Surface condition | Cleaning only; no electroplating | Cleaning specification, residue limit, cosmetic zones and handling requirements |
| Inspection | 2D optical dimensional inspection | Controlled characteristics, setup, frequency, report format and acceptance limits |
| Quotation input | Drawing or physical sample | Revision authority, quantity, tolerances and approval evidence |
This distinction is important during sourcing. A sample can show geometry and provide a reference for quotation, but it does not replace a controlled drawing when critical dimensions, tolerances, datums or revision status govern production acceptance.
Progressive Die Review for the Pictured Geometry
Progressive die stamping moves strip material through a sequence of stations. A station may create an opening, trim an edge, form a feature or prepare the part for a later operation. The appropriate sequence depends on the released geometry and cannot be reconstructed reliably from a finished photograph alone.
For components with multiple openings and formed edges, Zhengna Technology reviews how the features relate to the datum scheme and to the strip progression. The drawing or sample review should identify:
- which openings and outside edges are functionally related;
- which surfaces or features establish the measurement datums;
- whether a formed edge, collar or embossed area has a controlled height or profile;
- where burr direction and edge condition matter to assembly or handling;
- whether forming changes the position or shape of a previously punched feature;
- whether cosmetic zones require protection during tooling, cleaning and packaging; and
- how part orientation and release from the strip affect the final inspection state.
These are engineering review points rather than published tolerance promises. Tool station count, die layout, press selection and in-process controls are set only after the part authority, material condition, quantity and acceptance plan are known.
Using 6061 Aluminum in a Stamped Part
The confirmed material family is 6061 aluminum. The exact temper has not been supplied, so formability, bend response and springback must be reviewed against the specified material condition instead of assumed from the alloy name alone. A quotation should identify the applicable alloy designation, temper, thickness tolerance and any approved material alternative.
The photographed geometry includes cut openings and formed features. Their manufacturability depends on relationships such as edge distance, corner radii, forming direction and the sequence between punching and forming. If a critical opening must maintain its position after a nearby forming operation, the drawing should make that relationship explicit and define the inspection state.
The confirmed thickness is 1.5 mm for this product record. It is not a universal capability range or a statement that every feature retains nominal thickness after forming. Any local thinning, flatness, profile or formed-height requirement must be defined for the actual component.
Cleaning Without Electroplating
The confirmed post-process instruction is cleaning only, with no electroplating. This prevents an unsupported coating claim and keeps the quotation focused on the delivered surface condition. The RFQ should still explain what “clean” means for the project.
Useful requirements may include visible oil or residue limits, water-mark expectations, protected cosmetic areas, handling after cleaning, packaging material and the condition in which inspection occurs. If a buyer requires a named cleaning chemistry, cleanliness test or corrosion-protection method, it must be stated and reviewed separately. This page does not claim anodizing, conversion coating, plating or a particular cleanliness result.
What 2D Optical Inspection Can and Cannot Establish
The confirmed inspection method is a 2D optical measuring system. It can be suitable for accessible profiles, outside edges, hole locations, slot shapes and other projected dimensions when the part orientation, edge definition and measuring program are appropriate.
The method does not automatically establish material identity, formed height, three-dimensional profile, flatness, burr condition, surface cleanliness or every geometric relationship. A formed component may need an agreed fixture or another measurement method for characteristics that cannot be presented reliably in a two-dimensional view.
Before quotation, the buyer should identify:
- the dimensions and tolerances that are critical to function;
- the datum reference for each controlled characteristic;
- whether dimensions apply before or after forming and cleaning;
- which features require recorded numerical results;
- first-article, in-process and final-inspection expectations;
- sampling or full-inspection requirements, if any; and
- the report format and acceptance authority.
Zhengna Technology can then confirm which characteristics fit the stated 2D optical method and which require another agreed approach. No inspection result, capability index or lot acceptance is claimed here.
Drawing or Physical Sample RFQ Path
Zhengna Technology can begin quotation review from a drawing or a physical sample. A drawing provides revision, dimensions, tolerances and material authority directly. A physical sample can support geometry recognition and reverse-engineering discussion, but the quotation still needs an agreed definition of the controlled output.
Send the following information when available:
- controlled 2D drawing and 3D model, or a clearly identified physical sample;
- alloy 6061 specification and required temper;
- nominal 1.5 mm thickness and its tolerance;
- critical dimensions, datums, formed heights and profile requirements;
- burr direction, edge-break and cosmetic requirements;
- cleaning, residue, handling and packaging expectations;
- prototype, release and expected annual quantities;
- 2D optical measurement and report requirements;
- tooling ownership, validation and maintenance expectations; and
- mating or functional information needed to interpret critical features.
If quotation begins from a sample, the parties should agree how dimensions, tolerances, material condition and revision control will be established before production release.
Evidence and Capability Boundary
This product page combines the exact photograph with confirmed material, thickness, process, cleaning, inspection and quotation facts. It does not identify an automotive or other end use, and it does not claim a universal tolerance, press tonnage, tool life, production speed, inspection frequency or delivery time.
For the broader sourcing route, review custom stamping parts. Buyers assessing tooling, burr, plating and production-transfer responsibilities can also use the progressive stamping supplier audit guide.
Request a Quotation Review
Send the controlled drawing or physical sample, alloy and temper, quantity, critical dimensions, surface condition and inspection requirements. Zhengna Technology will review the manufacturing and quotation scope against the actual component.
Frequently Asked Questions
What material and thickness are confirmed for these components?
The confirmed product record is aluminum alloy 6061 at 1.5 mm thickness. The temper, thickness tolerance and document requirements must be defined in the RFQ.
Are the pictured parts plated?
No electroplating is specified. The confirmed post-process condition is cleaning only. Any detailed cleanliness, surface or packaging requirement remains project-specific.
Can 2D optical inspection measure every feature?
No. It is suitable for features that can be presented and measured reliably in the approved setup. Formed height, three-dimensional profile or other characteristics may require another agreed method.
Can Zhengna Technology quote from a physical sample?
Yes. Quotation review can start from a physical sample or a drawing. A sample-based project still needs an agreed material, dimension, tolerance, revision and acceptance definition before production release.